How to Choose a CNC Gundrilling Machine?
Selecting a Cnc Gundrilling Machine is a production decision, not just a spindle-speed comparison. The right machine must hold hole position, control chip flow, and keep coolant moving through a long, narrow bore. A small mismatch can leave chatter marks, a wandering drill, or costly rework. Deep holes expose weaknesses quickly.
Grand View Research’s CNC Machine Market report estimated the global market at USD 83.99 billion in 2023, with projected growth through 2030. This figure covers CNC machines broadly, not gundrilling equipment alone. It does, however, show the scale of investment in precision manufacturing. For buyers, the more useful evidence is often application-specific: hole diameter and depth, material, tolerance, batch size, and required cycle time. Reports from manufacturers and machine builders can help, but their claims should be checked against your own part drawings and trial cuts.
Quality expert W. Edwards Deming wrote, “Quality comes not from inspection, but from improvement of the production process.” That principle matters here. Choose a machine that supports a stable process, not merely an impressive specification sheet. Compare spindle rigidity, pressure and filtration capacity, tool support, automation options, and local service. Ask for a test cut using your material. Watch the chips. Measure the bore. One uncomfortable truth: the most expensive machine may still be the wrong one. A careful selection begins with the hole, not the brochure.
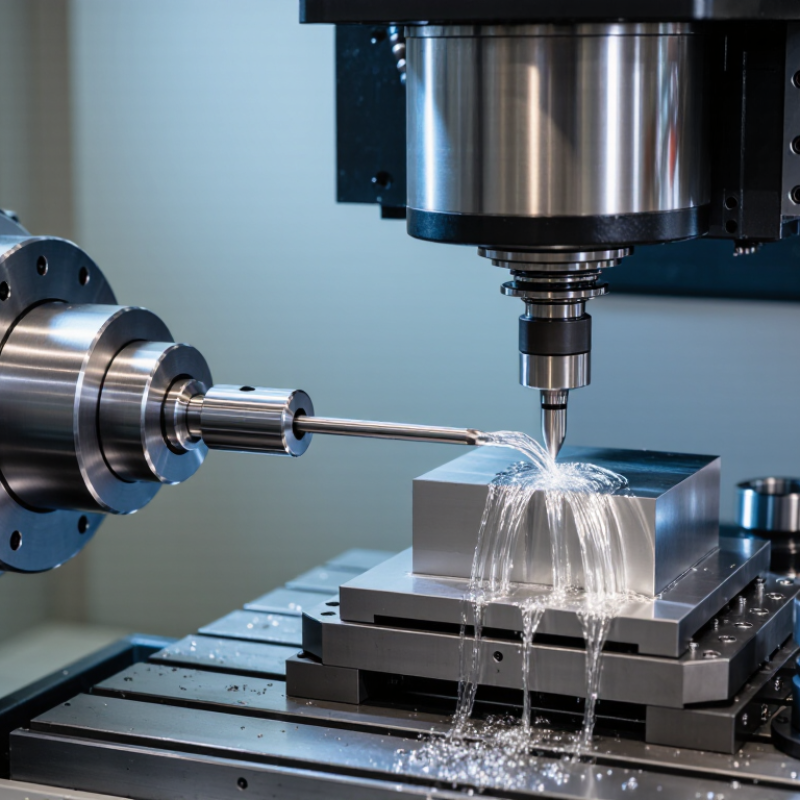
Table of Contents [Hide]
Understand the Workpiece and Hole Requirements
Before comparing CNC gundrilling machines, define the hole—not just its diameter. Record the finished diameter, depth, tolerance, straightness, and surface-finish requirement. A hole 12 millimeters wide and 300 millimeters deep has a 25:1 depth-to-diameter ratio. That is a very different job from drilling a short clearance hole. Deep-hole drilling references commonly treat ratios above 10:1 as requiring specialized methods. Use that benchmark as a prompt, not a guarantee: material, coolant delivery, and tool design also matter.
Describe the workpiece precisely. Include its alloy, hardness, heat treatment, shape, and whether the drill enters a flat or angled surface. A long, narrow hole in hardened steel can demand more rigidity and chip control than the same hole in aluminum. Check the available stock length and clamping points, too. A thin-walled part may distort under clamping pressure. Small details matter. The U.S. Census Bureau’s 2022 Annual Survey of Manufactures reports manufacturing value added at roughly $2.9 trillion, underscoring the scale of production where process variation carries real cost. That figure does not select a machine; your part data does. I would verify the drawing’s tolerance stack before requesting quotes—shop drawings sometimes leave the entry condition unclear.
How to Choose a CNC Gundrilling Machine? - Understand the Workpiece and Hole Requirements
| Selection factor | Workpiece or hole requirement | What to check when choosing the machine |
|---|---|---|
| Hole diameter | Specify the finished diameter and its tolerance. Small-diameter holes generally require a suitably sized drill, guide bushing, and stable setup. | Confirm the machine’s supported tool-diameter range and whether the required drill, coolant delivery, and guide arrangement are available for that diameter. |
| Hole depth and depth-to-diameter ratio | Calculate the ratio as hole depth divided by hole diameter. Deep-hole applications often have ratios above 10:1; the practical limit depends on diameter, material, tooling, and process conditions. | Check usable drilling stroke, tool length and rigidity, chip evacuation, and high-pressure coolant capacity. Ask for a trial cut or process validation at the required depth. |
| Workpiece material | Identify the material grade and condition, such as steel, stainless steel, aluminum alloy, or a heat-treated material. These can differ in machinability and chip formation. | Confirm suitable cutting parameters, tool geometry, coolant filtration, and chip-handling capacity for the actual material. Do not assume one setup suits every alloy or condition. |
| Hole straightness and position | Define the permitted deviation over the full hole length, along with the hole’s location relative to datum faces or other features. | Review machine alignment, workholding rigidity, entry-face preparation, guide support, and the inspection method. Verify capability on a representative workpiece. |
| Diameter tolerance and surface finish | State the required diameter tolerance and surface-finish value, including how and where they will be measured. | Determine whether drilling alone can meet the drawing requirements or whether a follow-up operation, such as reaming or honing, is needed. Confirm results with the specified measurement method. |
| Workpiece dimensions and mass | Record the workpiece’s length, width or diameter, weight, and the space required for fixtures and coolant access. | Compare these values with the machine’s work envelope, table or chuck capacity, loading access, and available support for long or heavy parts. |
| Hole layout and orientation | List the number of holes, their coordinates, entry directions, and any angled or intersecting holes. | Match the required axes and positioning range to the machine configuration. Consider rotary or indexing capability if multiple faces or orientations must be drilled. |
| Production volume | Estimate parts per shift or per year, holes per part, and expected changeovers between jobs. | For frequent or high-volume production, compare cycle time, tool-change arrangements, automation options, and setup repeatability. For varied low-volume work, prioritize flexibility and changeover access. |
| Coolant and chip management | Deep-hole drilling relies on effective coolant delivery and chip removal; requirements vary with hole size, depth, material, and cutting conditions. | Check coolant pressure and flow against the proposed process, plus filtration, tank capacity, temperature control, and chip conveyor or collection arrangements. |
| Final verification | Prepare a representative part or test coupon that includes the critical material, diameter, depth, tolerance, and hole orientation. | Use a cutting trial to verify cycle time, straightness, diameter, surface finish, and repeatability before committing to the production setup. |
Values and achievable results depend on the machine configuration, tooling, material, workholding, and process parameters. Confirm critical requirements with the machine supplier using the actual workpiece or a representative test piece.
Customers

Smart Robotics brand movie
Watch video